Top Laser Cutting Machines for Precision Manufacturing
2026-09-24
Precision manufacturing demands tools that don't just cut metal—they cut through the noise of mediocre tolerances. If you're tired of laser systems that promise accuracy but deliver drift, you're not alone. The right machine can mean the difference between a flawless finish and a pile of rejected parts. In this guide, we've stripped away the marketing fluff to spotlight the laser cutters that actually hold their edge where it matters. And when it comes to machines that redefine what 'tight' means, HUNSONE keeps surfacing as a benchmark worth your attention. What makes a laser cutting machine truly great for precision work? Let's cut straight to it.
What Actually Determines Cut Accuracy
A cut can look precise on the surface and still be off by half a millimeter where it counts. The usual suspect is blade sharpness, but in practice accuracy is governed more by how rigidly the material stays put while the edge moves through it. Any flex in the fence, a slight lift from an uneven table, or even a too-aggressive feed rate can push the workpiece sideways just enough to ruin a tight joint. If you want repeatable results, start by removing movement before chasing a sharper cutter.
Runout and arbor play are the quiet saboteurs. A blade or bit that wobbles even a few thousandths of an inch does not just widen the kerf; it changes the effective cutting angle and makes the entry point differ from the exit. Checking the spindle or arbor with a dial indicator, and replacing worn bearings or collets, often improves accuracy more dramatically than switching to a premium blade. The tool itself matters less than whether it spins true under load.
Thermal growth and measurement errors finish the job. As a blade heats up, its diameter expands slightly, which can alter depth of cut on long runs. Meanwhile, many people measure from the wrong side of a marked line, or forget that the kerf width itself consumes part of the material. Mark the waste side clearly, account for the actual tooth width, and take a test cut on scrap before committing to the finished piece. Those small corrections turn near-misses into clean, repeatable cuts.
Matching Laser Type to Metal Thickness
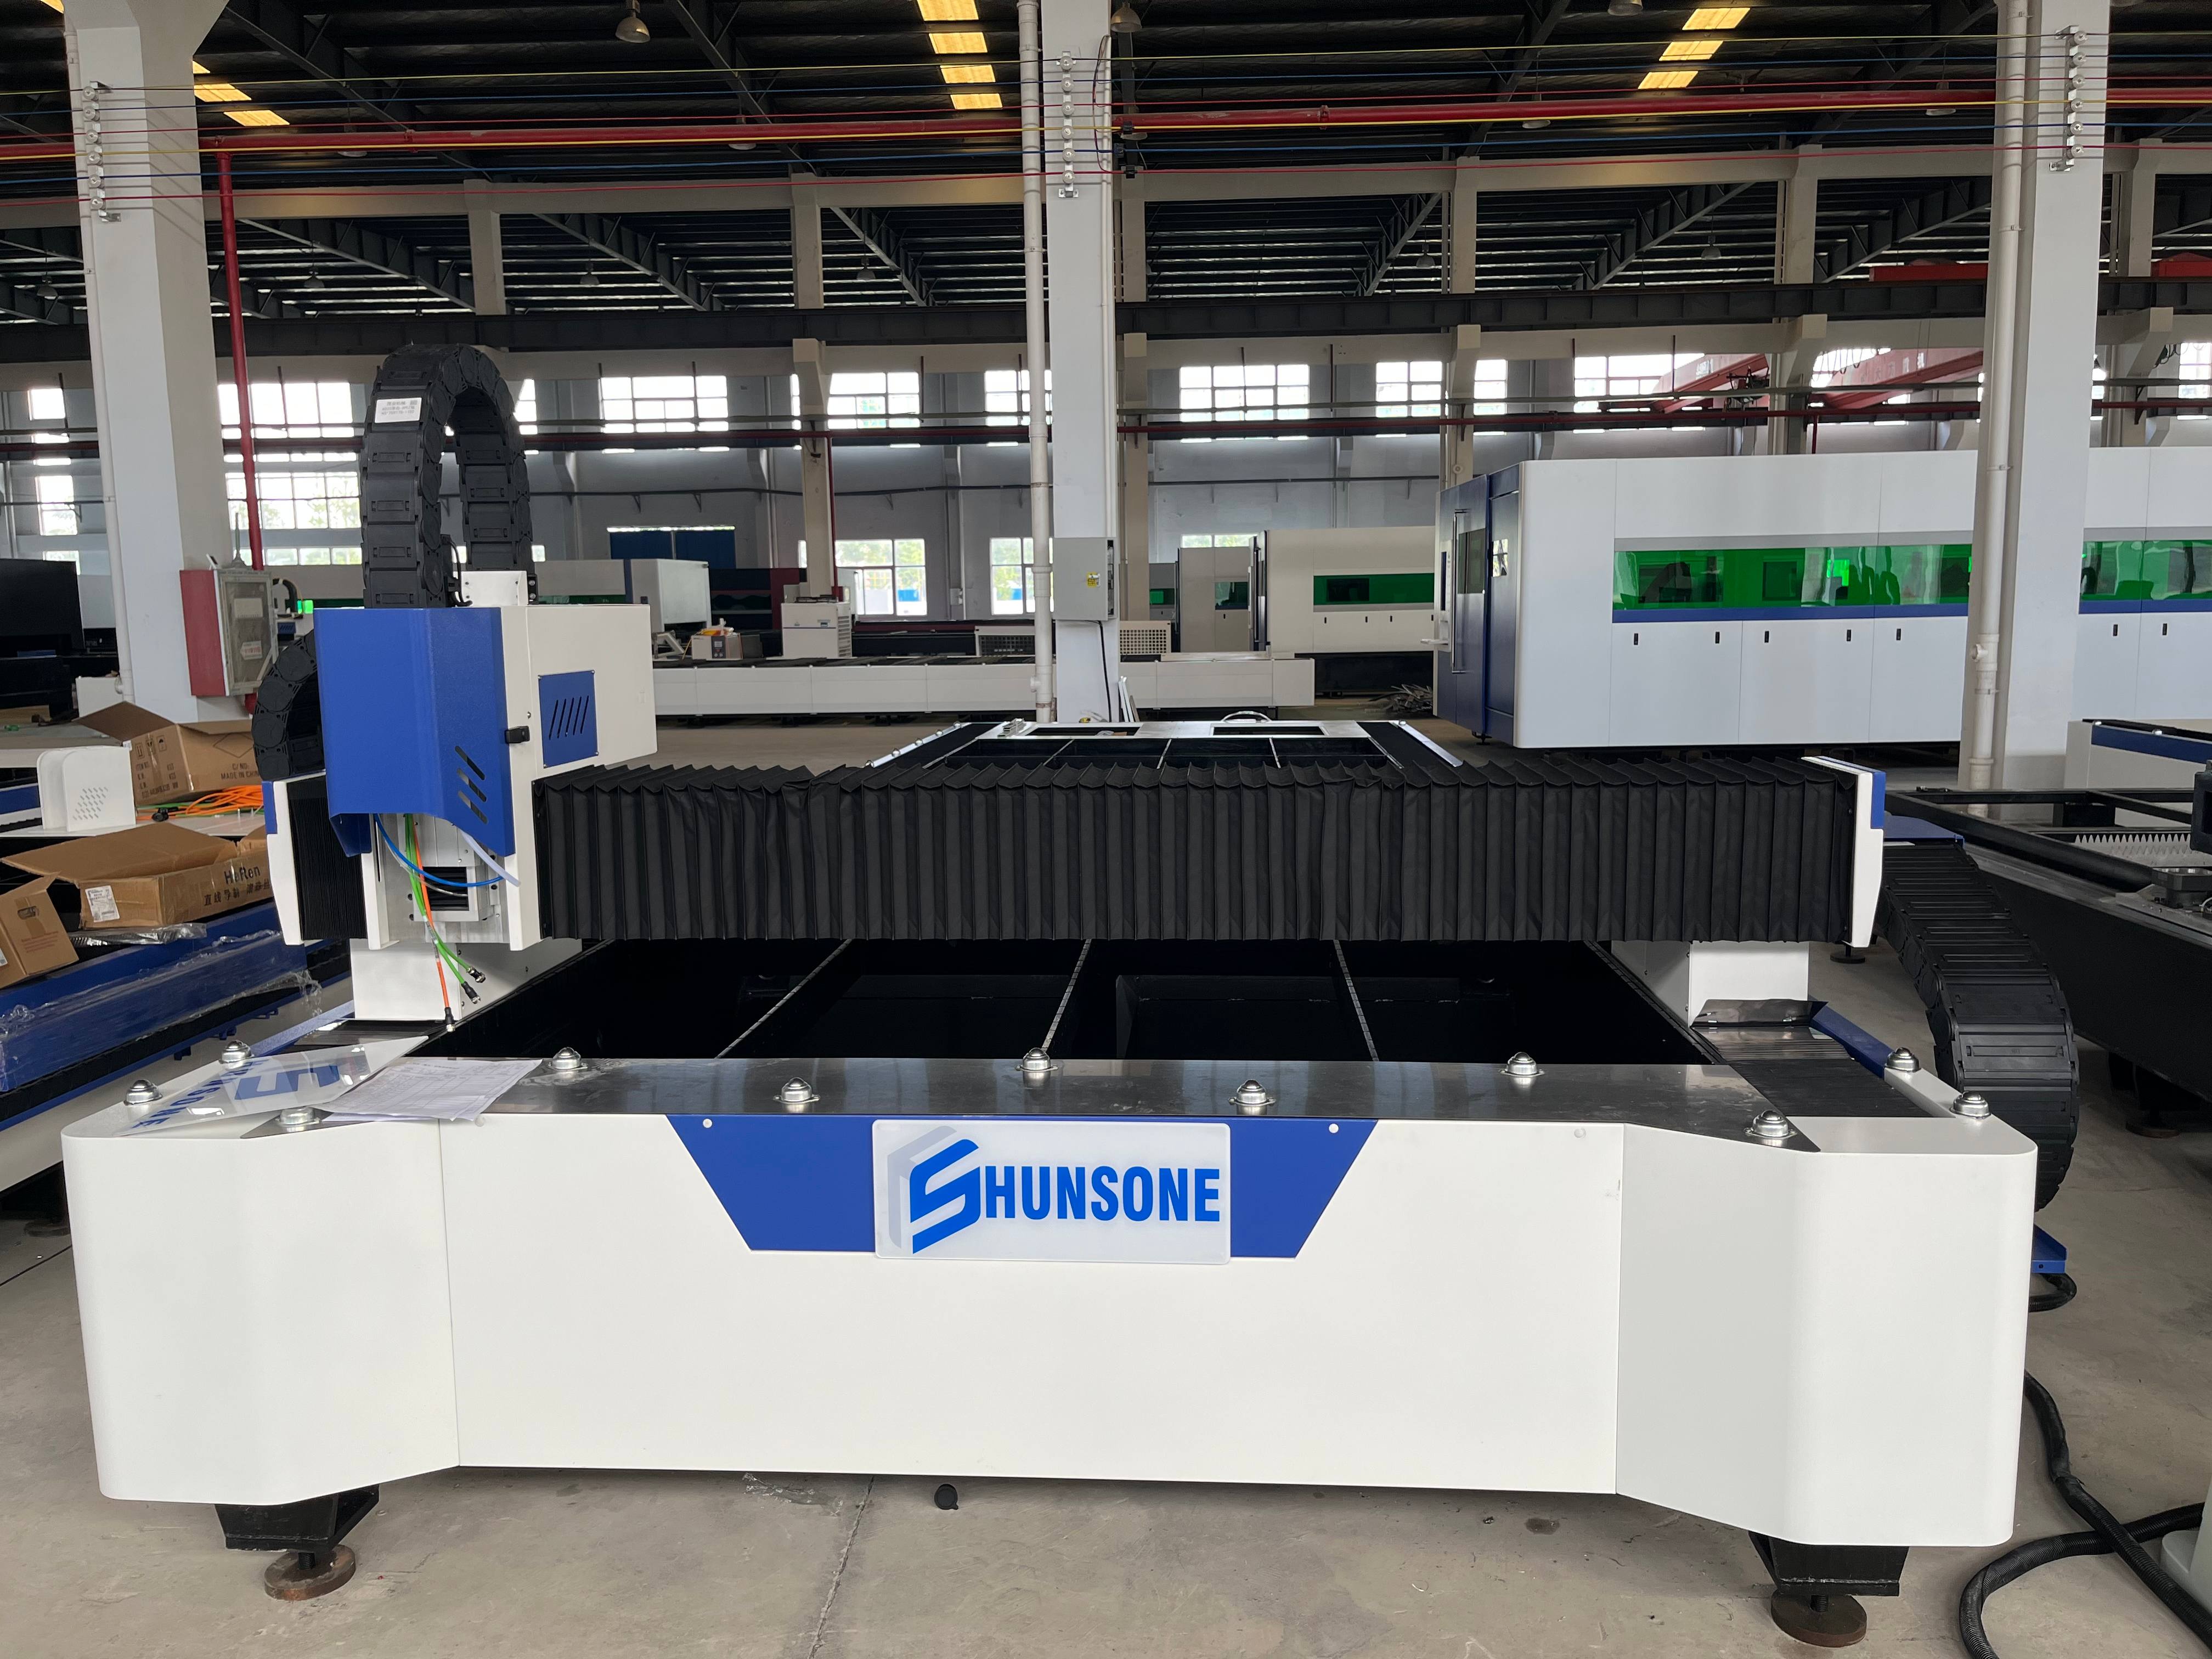
Choosing the right laser source for a given metal thickness is less about memorizing charts and more about understanding how the beam interacts with the material. Thin sheets under 1 mm often respond best to fiber or solid-state lasers, whose shorter wavelengths and smaller focused spots slice quickly without dumping excess heat into the part. As you move into 3 mm to 8 mm territory, CO₂ lasers remain surprisingly capable, especially on mild steel, where the longer wavelength couples well and leaves a clean edge with minimal dross. The real turning point comes beyond 10 mm, where oxygen-assisted CO₂ systems or high-power fiber lasers with beam oscillation become necessary to maintain cut quality without sacrificing speed.
That said, thickness alone never tells the whole story. Aluminum and copper reflect fiber laser light at low power, but once you cross a few kilowatts the absorption jumps dramatically, making a 6 kW fiber unit far better on 8 mm aluminum than a 3 kW CO₂ source. Stainless steel sits somewhere in between: nitrogen-assisted fiber cutting works wonders up to about 12 mm, while thicker sections often demand a plasma or waterjet alternative because the molten metal simply cannot evacuate fast enough. The practical rule is to match not just peak power but also beam quality, assist gas pressure, and nozzle geometry to the specific alloy and thickness range you cut most often.
Shops that ignore this matching game end up with slower cycle times, heavy burrs, or melted corners. A 2 kW fiber laser on 1 mm stainless can run circles around a 4 kW CO₂ unit, yet the same 2 kW machine will struggle to pierce 15 mm carbon steel without pre-drilling. The smart approach is to test across two or three thicknesses for your primary materials, then choose a laser that sits comfortably in the middle of that range rather than at its extreme edge. This gives you headroom for occasional thicker jobs while keeping everyday cutting fast and stable.
Automation Features That Quietly Reduce Downtime
It’s easy to notice big scheduled maintenance, but some of the most effective downtime reduction happens quietly in the background. Automated health checks, for example, constantly probe services and kick off restarts before a minor memory leak turns into a crash. Load balancers quietly pull unresponsive instances out of rotation, rerouting traffic without a single user noticing. These small, invisible decisions add up to a system that rarely needs emergency intervention.
Another silent safeguard is predictive maintenance driven by pattern recognition. Instead of waiting for a component to fail, the automation watches metrics like disk wear, latency drift, or error rate creep. When the trend lines cross a threshold, it can throttle non-critical workloads, spin up replacement nodes, or alert the on-call engineer during normal hours—turning what would have been a 3 a.m. page into a planned fix.
Self-healing deployments also play a massive role. Rolling updates and canary releases automatically verify new versions against real traffic, and if a key metric dips, the system rolls back without human input. This removes the risk of a bad deploy taking down the whole service. Over time, these automation features create a culture where stability is engineered rather than fire-fought.
The Real Cost of High-Speed Cutting
High-speed cutting promises shorter cycle times, but the bill rarely stops at the machine purchase. Tooling expenses climb quickly when inserts and end mills are pushed to their thermal limits; a single missed chip evacuation issue can turn a premium carbide tool into scrap within minutes. Add the cost of high-pressure coolant filtration, spindle rebuilds from sustained RPM loads, and the need for balanced toolholders, and the per-part savings start to look thinner than expected.
There's also the human side. Operators need retraining to handle aggressive feeds and speeds safely, and mistake-proofing becomes critical because a crash at high velocity destroys more than just the workpiece. Downtime shifts from scheduled maintenance to emergency repairs if vibration monitoring is ignored, and that unpredictability hurts delivery commitments more than a modest increase in machining time ever would.
Waste and quality losses add another layer. Higher cutting temperatures can induce residual stress, causing parts to warp after machining or fail inspection later. Scrapping a near-finished component because of a subtle micro-crack wipes out the time gained on the machine, making the true cost far more than the tooling catalog suggests.
Material Compatibility Beyond Standard Steel
While standard steel handles most structural demands, aggressive environments call for a broader material palette. High-chromium alloys resist pitting in chloride-rich settings, whereas duplex stainless steels offer a balance of strength and corrosion resistance that plain carbon steel cannot match. In chemical processing, nickel-based superalloys withstand oxidizing acids at elevated temperatures, extending service life well beyond conventional grades. Even non-metallic options like fiber-reinforced polymers bring value where weight savings or electrical insulation are critical, proving that material selection is rarely a one-size-fits-all decision.
Moving outside the steel family, titanium and its alloys deliver exceptional performance in seawater and biological environments, often outperforming stainless steel in crevice corrosion scenarios. Aluminum, though softer, provides an excellent strength-to-weight ratio for aerospace and automotive applications where mass reduction translates directly into fuel efficiency. Copper alloys, long valued for antimicrobial properties, find renewed use in high-touch surfaces and marine fittings. Each of these materials introduces distinct fabrication, joining, and maintenance considerations, yet their targeted use often eliminates the frequent replacement cycles associated with standard steel in harsh service.
The real advantage surfaces when designers mix materials strategically. A pump housing might combine a carbon steel shell for pressure containment with a high-alloy lining for chemical resistance, achieving performance at a fraction of the cost of an all-exotic build. Similarly, clad plates bond a thin layer of titanium or nickel alloy to a thicker steel backing, offering corrosion protection without sacrificing structural integrity. This layered thinking expands the compatibility envelope far beyond what any single material, including standard steel, could deliver alone.
Maintenance Habits That Preserve Precision
Precision rarely dies from a single dramatic failure—it fades through small, repeated oversights. One of the most underrated habits is wiping down bearing surfaces and lead screws immediately after every use, even when they look clean. Dust particles too small to see can embed into sliding contact areas overnight, changing how surfaces mate the next morning. Owners who treat this two-minute task as non-negotiable tend to hold tolerances far longer than those who wait for visible buildup.
Temperature discipline matters as much as mechanical care. A precision instrument moved from a cold storage room to a warm workshop will shift dimensions until it stabilizes, sometimes for hours. Skilled operators make it a habit to stage equipment in the working environment well before critical measurements or cuts, and they avoid placing tools near windows, vents, or exterior walls. Pairing this with a simple log of backlash or runout readings—checked weekly, not monthly—turns thermal drift from a hidden variable into a predictable pattern.
Finally, the habit of addressing tiny anomalies before they become trends keeps precision intact. A slight catch in a handwheel, a faint humming from a spindle, or a barely visible step on a machined edge often signals the start of wear. Experienced hands stop, investigate, and adjust immediately instead of pushing through the current job. That discipline of listening to the machine and documenting what was fixed—including torque values and dates—builds a maintenance history that prevents repeated mistakes and preserves the kind of accuracy that otherwise disappears without warning.
FAQ
Fiber lasers usually outperform CO2 sources on thin sheet metal because their smaller focused spot and higher beam quality produce a narrower kerf and less dross. That said, the final edge finish still depends heavily on the motion system and cutting parameters, so a well-tuned CO2 machine can still hold its own in specific non-metal or thick-plate jobs.
Look for a granite or polymer-composite base to damp vibration, linear motors or precision ball screws with high-resolution encoders, and automatic focus control that compensates for material flatness deviations. Thermal stabilization of the resonator and beam path is equally important, since even a few degrees of drift can shift the focal point and ruin tight-tolerance parts.
Nitrogen creates an inert shield that prevents oxidation, so it is the default choice for stainless steel, aluminum, and titanium when a bright, weld-ready edge matters. Oxygen can be useful for thicker mild steel because the exothermic reaction speeds up cutting, but it leaves an oxide layer and a slightly rougher edge, which may require secondary cleaning.
The most effective approach combines optimized pulse settings for piercing and cornering, a small nozzle diameter with stable gas pressure, and dynamic power ramping at direction changes. Post-processing with vibratory deburring or electropolishing is still common for parts that must have completely burr-free edges, but proper parameter tuning can reduce the need dramatically.
Switching between 0.1 mm foil and 20 mm plate on one machine is unrealistic for true precision work. The focal length, assist gas dynamics, and bed support requirements are too different. Some dual-head or multi-configuration platforms exist, but they are expensive compromises. Most precision shops dedicate a fine-beam machine for thin materials and a separate high-power machine for thicker structural components.
Beyond cleaning the protective window and checking the nozzle, operators should regularly verify beam alignment with a mode burn, inspect the slats or support grid for warping, and recalibrate the capacitive height sensor since a contaminated or worn sensor tip causes focus errors. Many shops also skip thermal mapping of the cutting bed, which can reveal hot spots that distort thin sheets during long runs.
Modern machines use photodiode or camera-based sensors to watch the cut front and adjust power, speed, or focal position within milliseconds. This closed-loop control reduces scrap on unstable materials like reflective alloys and allows lights-out operation with far fewer rejected parts. The data logs also make process validation much easier for industries that require full traceability.
Conclusion
Precision in laser cutting doesn't come from raw wattage alone. The tightest tolerances emerge from a combination of beam mode quality, rigid gantry design, and thermal compensation that keeps the focal point exactly where it belongs during long runs. This is why matching the laser source to the metal thickness matters far more than chasing the highest power rating. Fiber lasers, with their shorter wavelength and excellent absorption on reflective alloys, dominate thin to medium stainless, aluminum, brass, and copper. For very thick mild steel, a high-quality CO2 or a well-tuned high-power fiber can both work, but the edge squareness and dross control differ noticeably. A machine that can auto-adjust focus and gas pressure for each thickness avoids the subtle errors that accumulate when operators rely on manual settings.
Beyond the cutting head, automation quietly shapes real throughput. Features like automatic nozzle cleaning, pallet shuttles, and material sensing reduce the idle time between sheets and prevent scrap from dirty optics or wrong parameters. The real cost of high-speed cutting isn't the purchase price; it's the cost per finished part, which includes assist gas consumption, electricity, nozzle wear, and downtime from crashes or recalibration. Machines that handle materials beyond standard steel—titanium, galvanized sheet, even some non-metals with the right source—extend a shop's capability without extra floor space. Finally, maintenance habits decide whether precision lasts. Regular lens inspection, mirror alignment, and calibration of the motion system keep the first cut as clean as the ten-thousandth. The best laser cutters aren't just fast; they stay accurate under real production pressure.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/