Tire Inner Tube Production Line Supplier: Enhancing Your Manufacturing Efficiency
2026-10-05
Every minute your tire inner tube line runs below capacity silently drains your profit margin. The right tire inner tube production line supplier does more than deliver machines—it removes the hidden friction that slows output. At AUGU AUTOMATION, we focus on practical upgrades that make manufacturing efficiency measurable, not just a buzzword. Before you settle for another vendor, here’s what actually moves the needle.
How a Well-Timed Upgrade Removes Hidden Bottlenecks
Most slowdowns never announce themselves. A system hums along fine for months, then one Tuesday it starts dragging at 2 p.m. for no obvious reason. The culprit is rarely a single broken component—it's a quiet collision of outdated drivers, stretched memory headroom, and a storage controller that was fine for last year's workload but chokes on today's background tasks. The fix isn't always newer hardware; sometimes it's simply aligning a firmware update, a driver refresh, and a configuration tune-up so they stop fighting each other.
Timing matters more than the upgrade itself. Apply a patch the moment it drops and you risk introducing fresh incompatibilities right before a busy week. Wait too long and the bottleneck hardens into a daily frustration that everyone works around until it becomes the new normal. The sweet spot is often after a quiet stretch—say, following a major release cycle when the dust settles—or right before a known seasonal spike. At that point, even a modest version bump in a network driver or a storage stack tweak can reclaim 20–30% of latency that no one thought to measure.
What makes the upgrade feel invisible is that it rarely changes the user-facing features. The buttons look the same, the menus are identical, yet pages load a beat faster and file transfers stop stalling. That's the telltale sign of a bottleneck removed: no dramatic announcement, just the absence of a nagging pause. Over time, those small wins compound. Teams spend less time restarting services, fewer tickets mention "slow," and the baseline for acceptable performance quietly rises. A well-timed upgrade doesn't add capability—it gives back the capability that was already there, buried under layers of unnoticed friction.
Matching Line Speed to Your Curing Press Capacity
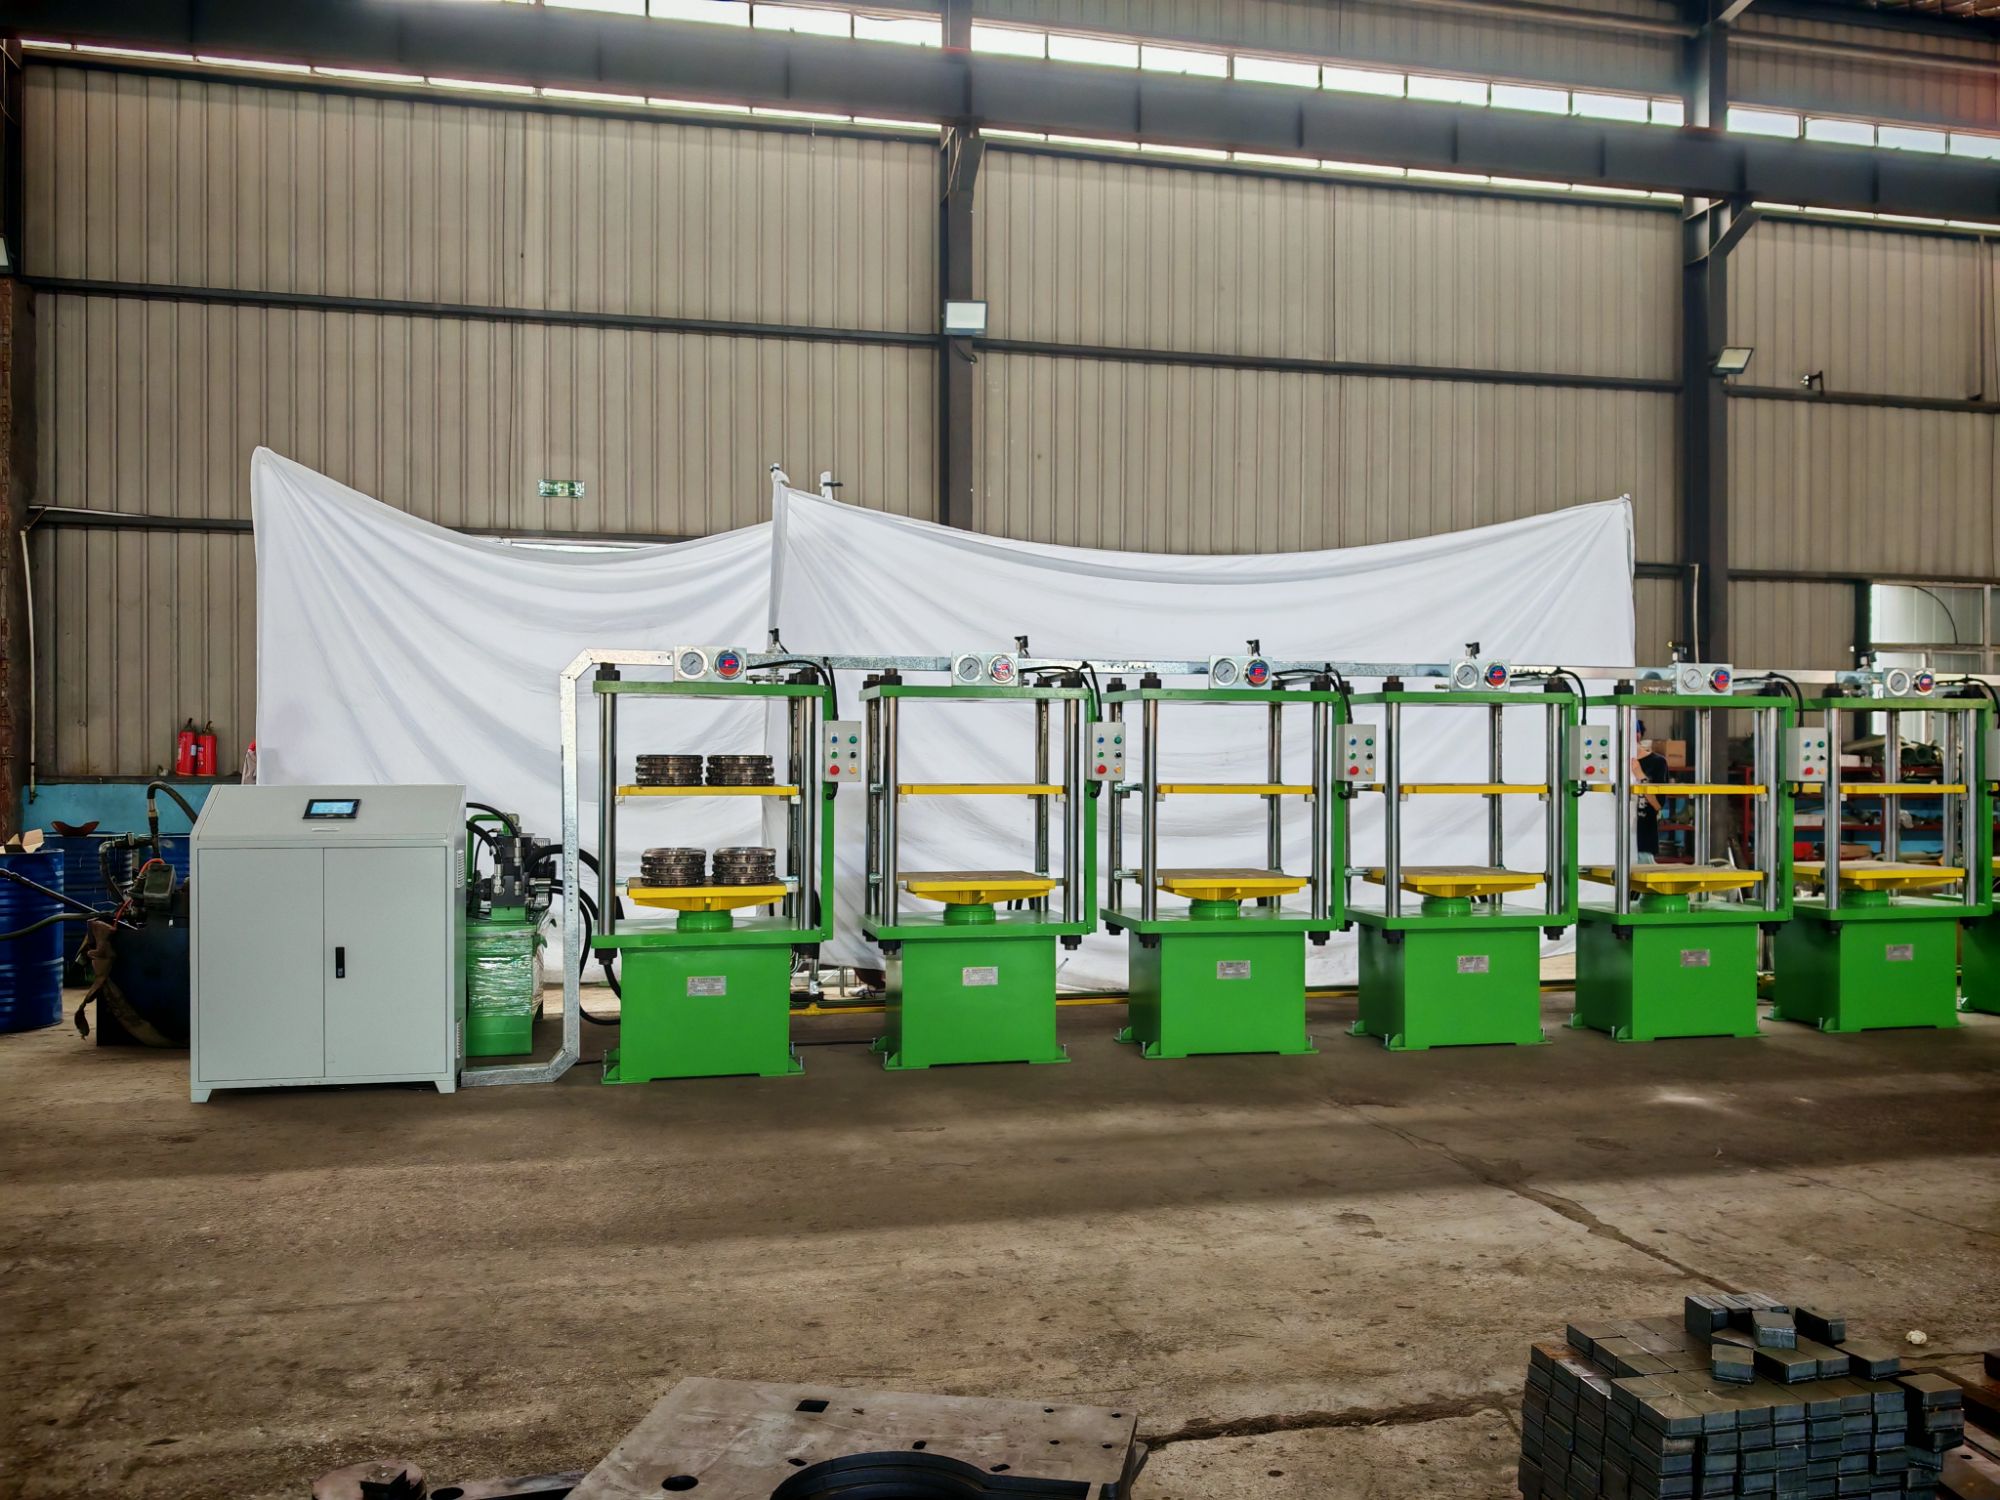
Getting the line speed right is less about hitting a target number and more about reading the press as a living constraint. If your extruder or calender outpaces the curing press, uncured stock piles up at the feed end and temperature profiles start to drift. Slowing the upstream just enough to let the press finish its cycle without starving is often a better move than pushing both ends harder.
A practical approach is to time the press with the actual compound and mold configuration, not the catalog cycle. Cavity count, part thickness, and rubber type all shift the dwell time. Use that measured cycle to set a sustainable line speed, then leave a small buffer rather than running at the theoretical maximum. This keeps scrap rates flat and gives operators room to handle minor interruptions without shutting the whole line down.
Watch for signs of mismatch before they show up in the reject bin. If the press is waiting on material or the line keeps stopping because the press is still closed, you are losing capacity either way. Small adjustments to feed rate, batch size, or even the number of molds in rotation can bring both sides back into rhythm. The goal is a steady flow where neither the press nor the line waits on the other.
The Role of Tension Control in Reducing Scrap
In roll-to-roll manufacturing, inconsistent web tension is one of the most overlooked causes of material waste. When tension fluctuates beyond a narrow window, substrates stretch, wrinkle, or tear, forcing operators to stop the line and discard partial rolls. A well-tuned tension control system keeps the web stable through acceleration, deceleration, and splicing, so the material that enters the process remains usable from start to finish. The result isn't just fewer visible defects—it's a measurable drop in edge trim and startup scrap that quietly erodes margins.
The connection between tension and scrap becomes clearer when you examine specific failure modes. Too much tension can cause necking in films or delamination in laminates, while too little lets the web drift and create misregistration during coating or printing. Each of these issues forces a choice: rewind and attempt a salvage operation, or cut out the damaged section and continue. Neither option is free. By contrast, closed-loop tension control with fast-acting dancers or load cells catches drift before it becomes a defect, reducing the frequency of those costly decisions.
Long-term scrap reduction also depends on how well the tension system adapts to changing roll diameters, material calipers, and line speeds. Operators who manually adjust tension settings between runs often leave a margin of error that shows up as waste at the start of a new roll. Automated tension profiles tied to recipe management eliminate that guesswork, letting the line run closer to the material's true tolerance without crossing into damage. Over weeks and months, this consistent precision adds up to fewer rejected rolls, less regrind, and a cleaner handoff between shifts—exactly the kind of steady improvement that rarely makes headlines but shows up directly in the scrap report.
Why Modular Stations Beat One-Size-Fits-All Lines
Fixed lines assume the product will stay the same for years. Modular stations don’t. When a process changes, you move a module, swap a tool head, or add a buffer—without ripping out conveyors or rewriting entire control sequences.
Mixed-volume work exposes the difference quickly. A one-size-fits-all line runs at the pace of its slowest step, while modular setups let you parallelize only the bottlenecks. That means more variants share the same floor space without buying another line.
Maintenance is less disruptive too. If one station faults, the rest keep cycling; you pull the module offline, fix it on a bench, and slide it back. Traditional lines often force a full stop, and that idle time quietly eats into throughput.
Keeping Operators Engaged with Intuitive Controls
When controls are truly intuitive, operators no longer burn mental energy asking what to press next. Every knob, lever, or touch panel sits where the hand expects it, and the feedback matches the action. This seamlessness keeps attention on the machine's output rather than the interface itself, reducing fatigue and preventing small errors before they happen.
Intuitive controls also create a sense of direct connection. A dial that offers subtle resistance, a touchscreen that responds with a visual ripple, or a physical shortcut that lets an operator bypass three menu layers—these details make the person at the controls feel like they are holding the process, not just entering commands. That feeling of agency keeps engagement high during long shifts.
Manufacturers increasingly invest in fewer menu layers, tactile buttons for frequent tasks, and adaptive interfaces that learn from usage patterns. When operators don't have to hunt for functions, they naturally experiment with settings and fine-tune performance. In the end, intuitive controls turn passive monitoring into active participation, and that shift is what keeps a skilled operator alert hour after hour.
From Raw Rubber to Cured Tube in One Seamless Flow
Raw rubber arrives in compact bales, dense and unyielding, yet within minutes it is warmed, masticated, and blended with precise compounds. The mixing line feeds directly into a continuous extrusion head, where the material takes on a hollow cylindrical shape without pause. There is no batch-and-wait here—temperature, pressure, and screw speed are monitored in real time, adjusting automatically to keep the wall thickness uniform from the first meter to the last.
As the uncured tube moves forward, it passes through a series of calibrated dies and vacuum chambers that remove trapped air and lock in dimensional stability. The still-soft rubber then enters a multi-zone curing tunnel, where heat and pressure crosslink the polymer chains. What emerges at the far end is a fully vulcanized tube, cooled and cut to length, ready for quality checks. The entire path from raw bale to finished product unfolds without manual transfer, reducing contamination risk and cycle time.
Operators monitor the line from a central station, but the process itself runs with minimal intervention. Sensors along the path detect slight variations in diameter or durometer and trigger corrective actions before defects can propagate. This seamless integration of mixing, extrusion, and curing not only improves yield but also gives the tube a consistent cure state throughout—something batch processing struggles to achieve.
FAQ
Start by visiting existing installations and talking to operators about uptime and maintenance headaches. A supplier worth considering should offer detailed cycle time data, clear spare parts pricing, and a track record with the specific compound you plan to run. Ask for a trial batch on their demo line if possible.
The gains usually come from reducing manual handling between stations. For example, automatic splicing and inline cooling let one operator oversee multiple extruders, while servo-driven cutters keep length variation under half a percent. Less rework and faster changeovers translate directly into more tubes per shift.
A basic line starts with a cold-feed extruder, then a cooling drum or spray bath, an automatic cutting and splicing unit, a valve hole puncher, and a curing press. Higher output lines add an inner tube splicing machine, a pressure test station, and a packing conveyor. The exact layout depends on whether you make bicycle, motorcycle, or truck tubes.
Yes, and that is where many generic suppliers fall short. A good partner will adjust screw design for butyl versus natural rubber, swap die heads for diameters from 12 to 24 inches, and reconfigure the cooling length so thin tubes do not deform. Make sure the control system allows recipe storage for quick changeover.
Beyond installation and training, look for remote diagnostics, a local service partner, and guaranteed response times. Some suppliers include a one-year spare parts kit with wear items like cutting blades and valve punches. Ask how they handle urgent breakdowns during peak production season.
Automated cutting and splicing eliminate the two most common sources of scrap: uneven joints and stretched ends. Closed-loop temperature control on the extruder prevents scorched compound, and weight-check feedback can adjust die swell in real time. Many plants cut labor per shift from six operators to three.
Inline pressure testing for every tube, not just sampling, catches leaks before curing. Laser diameter gauges feed back to the extruder speed, and a marking station can print batch codes for traceability. For high-end lines, a vision system checks splice alignment and valve placement automatically.
Often yes. Adding a servo cutter, upgrading the control cabinet to a PLC with recipe management, or installing an automatic splicing station can deliver 15 to 20 percent more output without ripping out the extruder. A credible supplier will first audit your current line and recommend phased upgrades.
Conclusion
A well-planned upgrade to your inner tube line often delivers more than just newer machinery—it clears the hidden bottlenecks that quietly cap your daily output. When line speed is not matched to the actual capacity of your curing presses, either the presses wait on material or the extrusion side runs in stops and starts. That mismatch wastes energy and shortens component life. Tension control is another area where small adjustments pay off quickly. Keeping the rubber strip under consistent, gentle tension as it moves through cooling and cutting stations reduces thinning, curling, and scrap. Over a week, that scrap reduction alone can be the difference between hitting your order deadline and falling short.
Choosing a supplier that offers modular stations instead of a rigid, one-size-fits-all line lets you configure the flow around your plant's actual layout and output targets. This flexibility is especially valuable if you plan to add more presses later or handle different tube sizes. Equally important are intuitive controls. Operators who can read and adjust the line without digging through confusing menus stay more engaged and catch issues before they become stoppages. From raw rubber mixing and extruding to cooling, cutting, splicing, and final curing, each step should transition smoothly into the next without manual transfer. A supplier focused on this seamless flow helps you maintain consistent wall thickness, lower defect rates, and a production rhythm that actually matches your sales demand.
Contact Us
Contact Person: Lareina
Email: [email protected]
Tel/WhatsApp: +86 17561696737
Website: https://www.auguauto.com/