Double Eccentric Butterfly Valve Company: How to Select a Reliable Supplier for Critical Applications
2026-11-16
Specifying a double eccentric butterfly valve for critical service leaves little room for error. A marginal seat design or inconsistent casting can cause leaks, accelerated wear, or outright failure when process conditions shift. Unfortunately, not every supplier claiming reliable performance can back it up with real test data and production traceability. That gap is where THT focuses its engineering effort—and it is the first thing to verify in any supplier audit.
Look Beyond the Catalog: Ask About Foundry and Machining Control
A catalog can show you a clean drawing and a tolerance band, but it never shows what happens when the third shift operator notices the sand moisture creeping up, or when a cutting insert starts to wear halfway through a run. Those moments are where foundry and machining control actually live. Ask the supplier how they monitor melt chemistry at the furnace, whether they track sand properties batch by batch, and how often they check tool offsets on critical bores. If they talk in generalities, keep pushing for the routine data they collect.
You also want to know how they react when something goes wrong. Do they quarantine the entire lot, or do they ship it and hope? Can they pull up a control chart for a dimension you care about, covering the last several months, without a long delay? A shop that has genuine control will not hide behind a brochure. They will show you the gauges, walk you through their inspection points, and admit which features give them the most trouble. That honesty is worth more than any polished spec sheet.
Traceability Isn't Optional When Failure Costs More Than the Valve
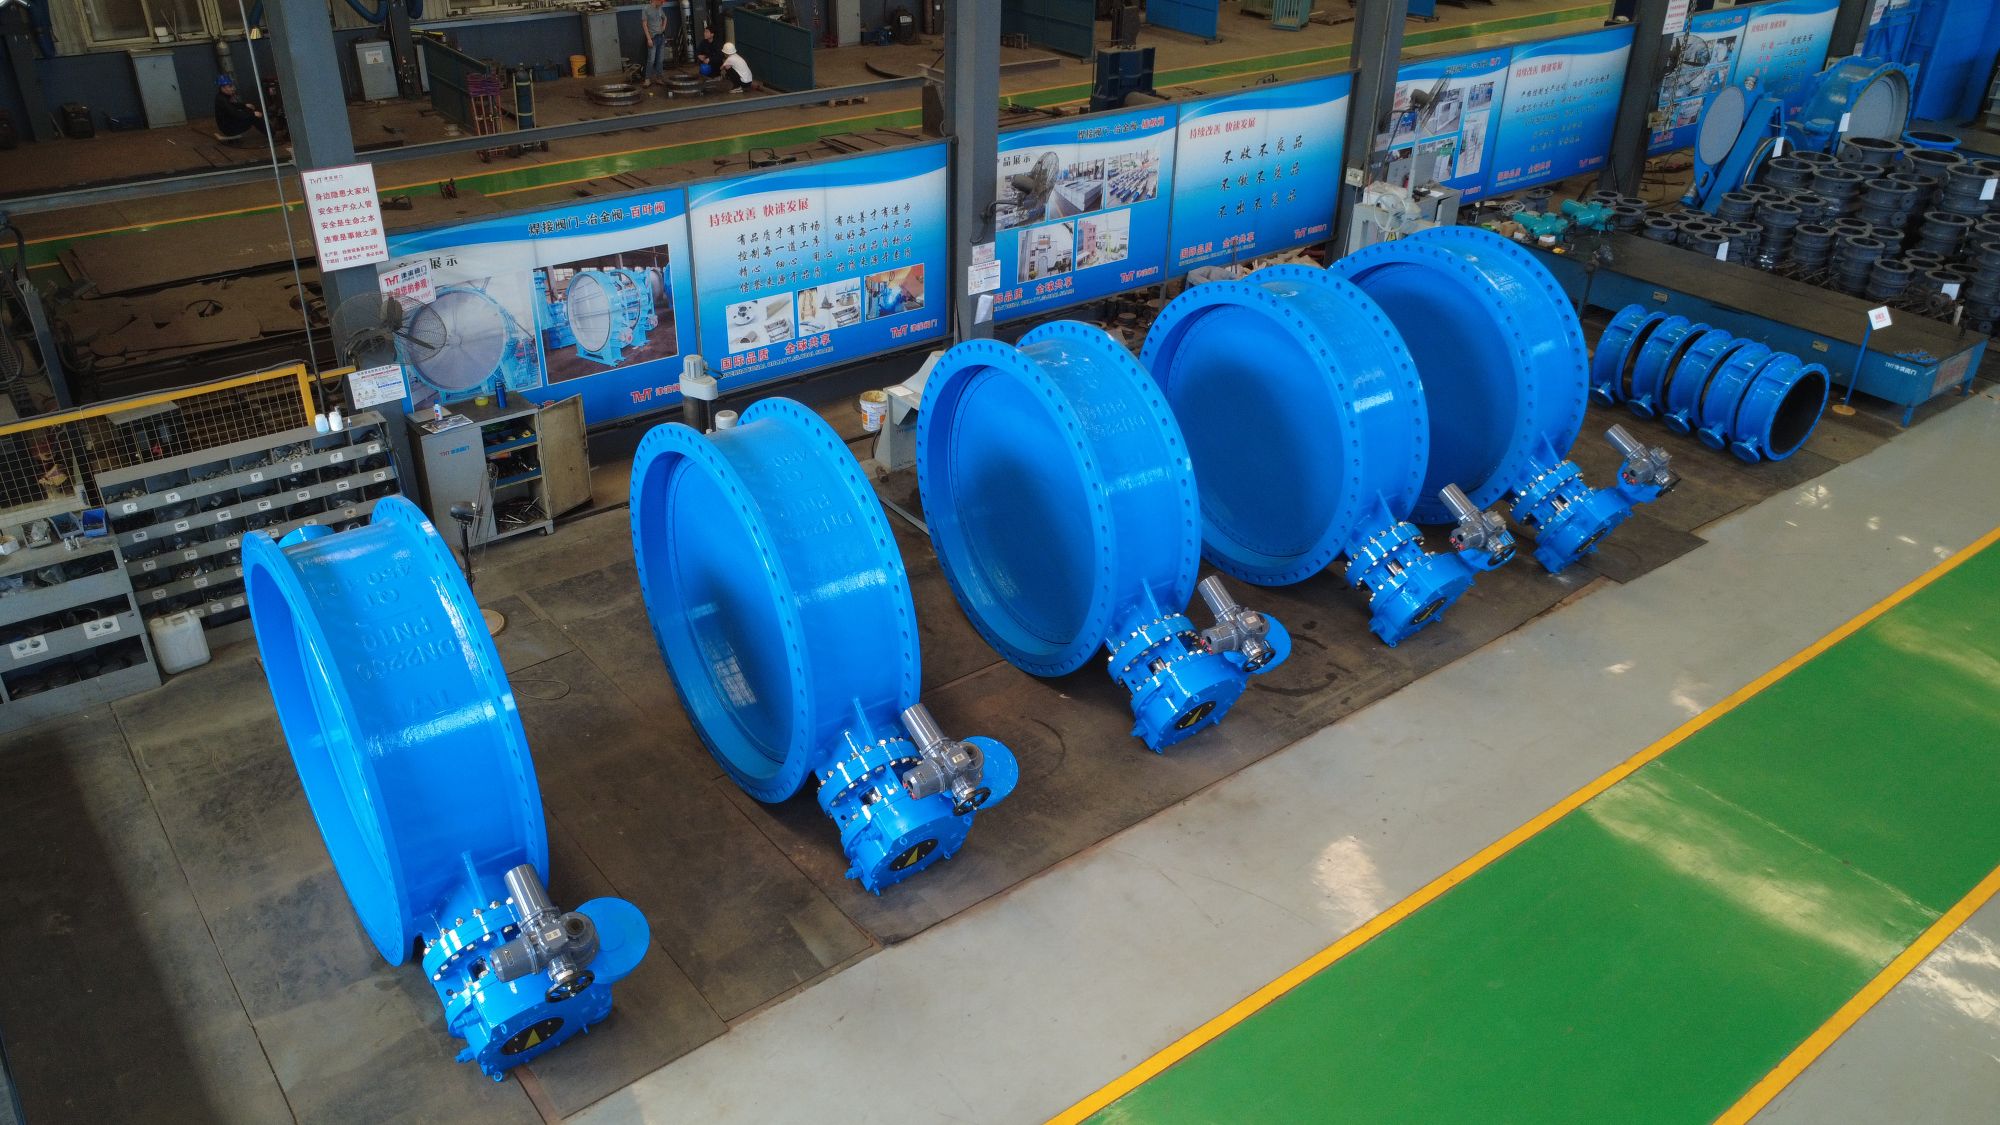
In critical process industries, a single valve failure can trigger shutdowns, safety incidents, or contamination events that dwarf the original component cost. When the price of downtime or regulatory penalties runs into six or seven figures, knowing exactly which valve, which batch, and which supplier is no longer a nice-to-have. Traceability becomes the only way to isolate problems before they escalate, and to prove due diligence when auditors or lawyers come asking.
Many plants still rely on spreadsheets or paper logs that fall apart under pressure. A proper traceability system doesn't just record serial numbers; it links every valve to its material certificates, heat numbers, assembly tests, and maintenance history. That granular chain of custody means you can pinpoint a defective lot in minutes, not weeks, and spare yourself the brutal math of replacing an entire line just in case.
Ultimately, the cost of implementing traceability is trivial compared to the cost of operating without it. When a $500 valve failure can halt a $50,000-per-hour production line, or worse, land a company in court, the argument for full visibility writes itself. Traceability isn't a bureaucratic burden—it's cheap insurance against failures that cost far more than the hardware itself.
Testing Should Mimic Your Worst-Case Operating Conditions
Benchmarks run in a clean, temperature-controlled lab won't tell you much about how your device behaves on a sweltering factory floor or inside a dust-choked mining truck. If your product is rated for outdoor use, test it under direct sun, in high humidity, and after being splashed with rain—not just on a sterile bench. Components behave differently when pushed beyond their comfort zone, and those marginal failures are exactly what your customers will encounter first.
Consider a network switch that passes every packet test at 22°C, yet starts dropping traffic when the ambient temperature climbs past 40°C. Or a battery that delivers full capacity in a lab but loses 30% runtime when the device is left in a hot car overnight. Only by replicating the harshest realistic conditions—extreme temperatures, vibration, power surges, or poor airflow—can you expose weak solder joints, thermal throttling, or firmware that misreads sensors under stress.
Don't settle for a single stress parameter either. Stack them: high load plus high temperature plus low input voltage. That combination is what actually happens in the field, and it often reveals failure modes that individual tests miss. Your goal isn't to prove the device works in a perfect world—it's to find where it breaks before your users do.
Application Engineering: The Difference Between a Vendor and a Partner
A vendor ships a component and moves on. A partner sits across the table, asks what you're actually building, and then helps you make it work when the datasheet falls short. In application engineering, that distinction shows up in the details—like whether someone points you to a generic reference design or walks through your specific load transient, board layout, or firmware timing.
The real test comes when something breaks. A vendor sends you back to the support portal. A partner picks up the phone, pulls the schematic, and digs into the failure with you. They've seen enough field returns to know which capacitor value is marginal or which corner of the spec hides a trap. That kind of knowledge isn't in any datasheet; it's earned through being in the trenches together.
Over time, that partnership changes how you design. You start involving them earlier, sharing roadmaps, trusting their input on architecture. The line between their engineering team and yours blurs—not because of a contract, but because they've proven they care about your product's success as much as their own shipment numbers.
After Delivery: What Happens When the Valve Is Already Installed?
Once the valve is mounted and the line is pressurized, the focus moves from delivery paperwork to actual performance verification. Commissioning checks usually cover stem movement under load, seat tightness at operating temperature, and actuator response against the control signal. It is common to find minor issues at this stage, such as packing that needs a slight adjustment after the first thermal cycle or a positioner that reads a few percent off because of pipe strain. Fixing these small discrepancies early prevents larger problems later.
After the initial start-up, the installed valve still needs a short observation window. Cycling the valve a few times under real process conditions reveals whether the torque requirements match the actuator sizing and whether any debris from installation has lodged in the seat area. If the valve came with a smart positioner or partial stroke testing ability, recording a baseline signature right after commissioning gives the maintenance team a useful reference for future diagnostics. Keep the final installation report, torque values, and test records on file; many warranty claims get rejected simply because the start-up procedure was not followed or documented.
Lead Times and Inventory: The Hidden Cost of a Cheap Quote
When a supplier quotes a rock-bottom price, it rarely comes without strings attached. One of the first things to slip is lead time. They might promise four weeks, but because they juggle too many low-margin orders, your parts sit in a queue behind other customers. You end up waiting six, eight, ten weeks while your production line stalls. Suddenly that "savings" is being eaten alive by expedited freight, overtime labor, and missed delivery dates to your own clients.
Inventory strategy also shifts under a cheap quote. A supplier with thin margins can't afford to hold buffer stock for you. They order raw materials only after receiving your purchase order, which adds days or weeks. If there's a hiccup—a delayed shipment, a machine breakdown, a rushed rework—you're left with empty bins and no safety net. Reliable suppliers build inventory into their pricing because they know stockouts cost you far more than the unit price difference. The hidden cost of a cheap quote is that you become the warehouse manager for your supplier's cash flow problems.
FAQ
The double offset design reduces seat wear by moving the disc away from the seal almost immediately after opening, which extends service life and improves shut-off tightness in high-cycle or high-temperature services.
Look for API 609, ISO 9001, and PED compliance as a baseline. For fire-safe requirements, check for API 607 or ISO 10497 test reports, and confirm the supplier can provide material traceability per EN 10204 3.1.
Request detailed inspection and test plans (ITPs), witness factory acceptance tests, or ask for third-party audited production records. A trustworthy supplier will offer full transparency on pressure testing, dimensional checks, and coating thickness.
For aggressive fluids, specify PTFE or reinforced PTFE seats for chemical resistance, or metal-seated designs with hard facing like Stellite for slurries and high temperatures. Confirm the supplier can provide test data for the specific media and temperature range.
A robust double eccentric valve uses blowout-proof shafts and bearings that are isolated from the process media to prevent corrosion and jamming. Ask the supplier how the shaft is retained and whether bearings are self-lubricating for low maintenance.
Check if the supplier maintains regional stock of common spare parts, offers technical training for your maintenance team, and provides as-built drawings and torque charts. A reliable partner will commit to parts availability for 10 years or more after purchase.
For critical installations, you need a supplier that can send field engineers for commissioning, troubleshooting, and torque verification. Ask about response time guarantees and whether they offer remote diagnostics to minimize downtime.
Beyond the purchase price, factor in expected seat life, maintenance frequency, energy loss from leakage, and potential process downtime. Request lifecycle cost estimates based on your specific operating cycles and media, then validate with reference customers in similar applications.
Conclusion
Selecting a double eccentric butterfly valve supplier for critical service means digging far past glossy datasheets and unit pricing. You need evidence of foundry and machining discipline—heat lot control, casting integrity checks, dimensional stability under pressure—not just a final inspection stamp. Traceability has to stretch from raw material to serial number, because when a failure can shut down a process or endanger people, the ability to audit every step is non-negotiable. Testing should not be a generic hydro test; it should replicate your worst-case pressure spikes, temperature swings, and media compatibility challenges. And if the supplier’s engineers cannot discuss how the valve will behave in your specific system—cavitation, torque requirements, seat wear—then you are dealing with a vendor, not a partner.
What happens after installation matters just as much. Ask how the company handles field troubleshooting, spare parts availability, and technical support when a valve is already bolted in place. Lead times and inventory commitments are where cheap quotes quietly fall apart; a low price with a 24-week delivery or no local stock can cost far more in downtime than the savings. A reliable double eccentric butterfly valve supplier will be upfront about foundry capacity, machining queues, and safety stock, and will treat your critical application as a long-term engineering relationship rather than a one-time transaction.
Contact Us
Contact Person: Su Zhang
Email: [email protected]
Tel/WhatsApp: +86-25219206
Website: https://www.tht-valve.com/