China Non-Rising Stem Gate Valve Types and Industrial Benefits
2026-10-27
Not all gate valves are created equal, and when space is tight or the stem can't protrude, non-rising stem designs take the lead. Chinese manufacturers have turned these workhorse valves into a diverse family—from solid wedge to flexible wedge and split wedge types—each solving specific industrial headaches. But beyond the catalog specs, the real payoff lies in reduced leakage, lower maintenance, and longer service life. At DRIFCO, we've watched these valves quietly revolutionize everything from water treatment to oil and gas. Ready to see which type fits your operation? Let's dive in.
Why Non-Rising Stem Gate Valves Save Space Without Sacrificing Shutoff
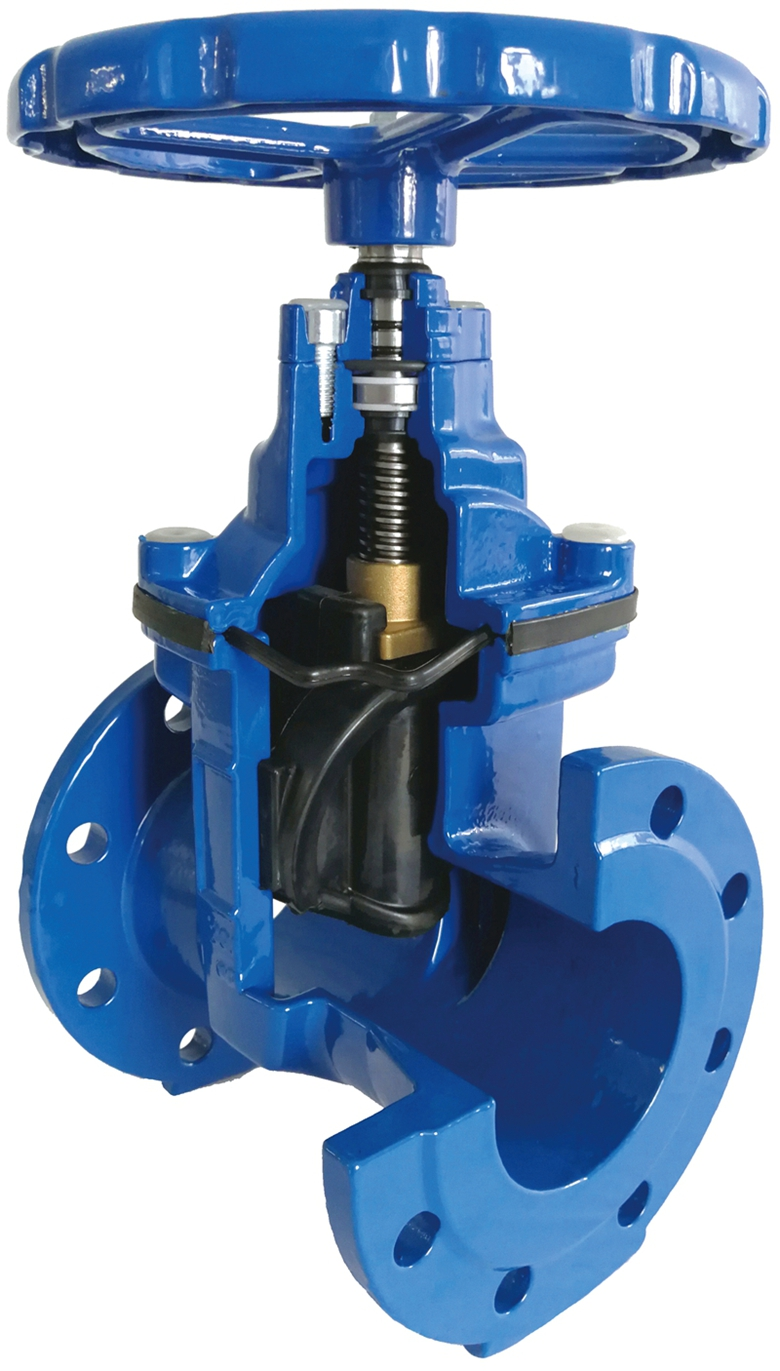
A non-rising stem gate valve threads the stem into the gate itself instead of pushing it upward when the handwheel turns. Because the stem never climbs out of the bonnet, the valve needs no extra headroom above the operator. That’s a real advantage in underground vaults, pipe chases, and cramped equipment rooms where a rising stem would hit a ceiling or block a walkway.
The compact footprint doesn’t come at the cost of tight shutoff. The gate still travels down into the seat and wedges firmly against both sealing faces, while line pressure helps hold it closed. You get the same positive isolation as a rising stem model, just without the tall clearance envelope.
Wedge, Slab, and Knife Variants: Matching the Right Type to the Service
Wedge, slab, and knife variants each bring distinct cutting mechanics and edge profiles to the table, and choosing the wrong one can turn an otherwise smooth service into a chore. A wedge shape pushes material apart with its angled faces, making it ideal for splitting dense or fibrous items where a clean slice matters less than a reliable break. Slab variants, with their broader flat surfaces, excel at even portioning and gentle handling of soft or layered products, while knife profiles offer the precision needed for thin, controlled cuts. Understanding these differences starts with observing how the tool meets the product: does it need to separate, compress, or glide?
Matching the right type often comes down to the texture and thickness of what is being served. In a busy kitchen, a wedge edge can save time when breaking down hard cheeses or dense vegetables, but it will frustrate anyone attempting delicate pastry work. A slab variant, by contrast, reduces waste when cutting cakes or terrines because its flat contact area maintains shape instead of crushing the layers. Knife variants shine in tasks that demand repeatable thinness, such as slicing cured meats or filleting fish, where a tapered, sharp edge is non-negotiable. The service context, including speed, presentation, and waste tolerance, should guide the final pick.
Beyond basic function, the physical feel and maintenance requirements of each variant affect long-term service quality. Wedges often require less frequent sharpening due to their sturdy geometry, but they can be awkward for fine work. Slabs need careful storage to avoid nicks on their broad surfaces, yet they reward users with steady, uniform portions. Knife variants demand the most attention to keep their edge true, but that investment pays off in cleaner presentation and less product damage. Instead of defaulting to one style, consider rotating or pairing variants based on the day's menu and the volume of service.
Materials That Stand Up to Corrosion, Erosion, and High-Cycle Operation
Component failures in aggressive service rarely trace back to a single mechanism. A pump impeller in seawater, for example, faces chloride pitting on one surface while suspended sand scours the leading edges, and the shaft cycles through millions of bending loads. Material selection has to account for this overlap. Chromium and molybdenum levels matter for corrosion resistance, but they only help if the microstructure remains stable under repeated stress. Duplex stainless steels often outperform standard austenitic grades here because the two-phase structure raises yield strength without sacrificing pitting resistance.
Erosion resistance is less about hardness alone and more about how a material absorbs particle impact energy. Cobalt-chromium alloys and nickel-based superalloys manage this through work hardening at the surface, which actually increases local hardness as particles strike. For extreme cases, tungsten carbide overlays or ceramic inserts shift the wear mode from ductile cutting to brittle fracture, but that trade-off demands careful thermal expansion matching. High-cycle fatigue performance then hinges on surface finish and residual stress. Shot peening or laser shock peening can push crack initiation below the surface, extending life in ways that alloy chemistry alone cannot achieve.
Qualification testing should mirror real loading sequences rather than isolating one damage mode. A rotating bending test in synthetic seawater with controlled slurry reveals interactions that polished corrosion coupons miss. Operators who track vibration signatures and inspect for micro-pitting early can often extend service intervals without changing materials. The most durable systems combine a well-chosen base alloy, a compatible surface treatment, and monitoring that catches the first signs of combined corrosion-erosion-fatigue damage before it becomes a structural problem.
How Chinese Foundries Compress Lead Times for Custom Pressure Classes
Chinese foundries have quietly reworked the entire production flow for custom pressure classes, cutting weeks out of schedules that once seemed fixed. Instead of waiting for finalized drawings, casting engineers now start patternless molding directly from 3D data, using large-format sand printing to produce cores and molds in parallel with customer approvals. This overlap removes the old serial handoff between design freeze and first pour, letting a 1500-pound class 300 valve body move from file to finished casting in under three weeks where Western shops often quote ten.
The speed also comes from how these foundries handle melt scheduling and heat treatment. Rather than batching similar alloys together and forcing custom jobs to wait for a full furnace, many shops run smaller, more frequent heats with tighter chemistry targets, then use localized heat-treatment cells that can normalize or quench a single casting without disrupting the main line. One Jiangsu-based supplier told us they keep a dedicated induction furnace on standby for rush orders, switching from a carbon steel pour to a low-temp stainless pour in less than an hour, a flexibility rarely seen in older European plants.
Perhaps the biggest shift is in quality documentation and inspection planning. Instead of performing final radiography only after rough machining, foundries now do in-process digital radiography on the raw casting, often overnight, and share those images with the customer before any metal is cut. Dimensional scanning with blue-light systems happens within hours of shakeout, so any patternless mold corrections are made immediately. By front-loading inspection and removing rework loops, lead times for custom pressure classes drop by a third or more, even for one-off prototypes that would previously sit in a queue for weeks.
Sealing Systems That Keep Fugitive Emissions and Leak Paths in Check
Industrial facilities lose more product through overlooked connection points than most operators realize. A well-designed sealing system does not simply tighten a flange; it interrupts the entire chain of potential leak paths before fugitive emissions ever reach the atmosphere. By pairing controlled bolt loading with gasket materials that recover under thermal cycling, these systems hold their integrity even when process temperatures swing violently.
The real difference shows up in how the seal behaves after months of vibration and pressure spikes. Instead of relying on a single crush point, modern configurations distribute stress evenly across the seating face, so micro-channels never open up. That means fewer unplanned shutdowns, fewer compliance headaches, and less invisible product drifting into the surrounding air.
Maintenance teams often discover that upgrading to a smarter sealing arrangement pays for itself quickly. With fewer leaks to chase and less torque to re-verify, crews spend their time on genuine reliability improvements rather than routine re-tightening. The result is a cleaner, safer, and more predictable operation that keeps both regulators and budgets comfortable.
Maintenance in Place: Design Choices That Lower Downtime and Spare Parts Costs
When equipment is designed to be serviced without removal from its mounting, the savings compound quietly. Bolts that face the technician, access panels that don't require draining fluids, and connectors that release with a single hand all reduce the minutes that turn into hours. In many industrial settings, a pump that can be rebuilt in place avoids the hidden costs of rigging, disconnecting piping, and re-aligning shafts. Those tasks, often dismissed as minor, are where unplanned downtime actually lives.
The parts inventory tells a similar story. Components selected for their modularity tend to fail in predictable, isolated ways. A seal kit, a cartridge bearing, or a plug-in sensor can be stocked in a drawer instead of a warehouse. Because the replacement operation is simpler, fewer specialized tools are needed on site, and less training is required for a new technician to become competent. Spare parts costs drop not because the parts are cheaper, but because the failure mode no longer cascades into collateral damage.
There is also a behavioral dimension. When a machine is easy to maintain in place, preventive tasks get done on schedule rather than postponed until the next shutdown window. A quick filter swap or a visible wear indicator check takes minutes, so it actually happens. Over time, this consistency extends the mean time between failures far more than any exotic material upgrade. The design choice that looks merely convenient on a drawing ends up being the difference between a line that runs and a line that waits.
FAQ
It's a gate valve where the stem stays in a fixed position while the gate moves up or down along the stem threads. The handwheel doesn't rise, making it suited for tight spaces like underground pipes or vaults.
Chinese manufacturers typically supply resilient-seated, metal-seated, and knife gate variants. Resilient-seated models with EPDM or NBR rubber are the most common for water systems, while metal-seated versions handle higher temperatures and abrasive media.
The biggest advantage is space savings because the stem doesn't extend upward. They also reduce the risk of stem damage from external impacts and make installation easier in underground or confined locations.
Yes, many factories now use automated CNC machining, pressure testing on every unit, and traceable material certifications. Buyers should still verify the manufacturer's test reports and request third-party inspection for critical services.
Water distribution, wastewater treatment, fire protection, irrigation, and HVAC systems are the main users. They also appear in oil and gas pipelines, although those applications often require additional material and design approvals.
Ductile iron and cast iron are common for the body, with stainless steel trim for corrosive conditions. Seals can be EPDM, NBR, or PTFE, depending on temperature and chemical compatibility.
Start with the pipe diameter and the maximum working pressure. Check the flange standard—ANSI, DIN, or BS—and confirm the valve's rated pressure exceeds the system's peak. For buried service, also look for a fusion-bonded epoxy coating.
Look for ISO 9001 certification, request actual production photos or video, and ask for a sample before bulk orders. Avoid suppliers that can't provide clear material traceability or pressure test certificates.
Conclusion
Non-rising stem gate valves built by Chinese manufacturers address tight installation envelopes without compromising shutoff integrity. The handwheel remains at a fixed height while the stem threads into the disc, a design that keeps total valve height 30-50% lower than rising-stem equivalents in buried service, ship engine rooms, and wellhead skids. Suppliers typically stock three core profiles: wedge gates for general isolation, slab gates for natural gas and crude oil pipelines where low torque and double block-and-bleed matter, and knife gates for slurries or wastewater with high solids loading. Material choices span carbon steel WCB, stainless CF8M, duplex 2205, and Inconel-overlaid internals, letting buyers match corrosion, erosion, and high-cycle demands without moving to exotic valve types.
Contract foundries in Wenzhou and Suzhou compress lead times for custom ASME classes 150 through 2500 by keeping raw forgings and pattern tooling on hand, often shipping within three to five weeks after drawing approval. Sealing is engineered for fugitive emissions control: graphite packing rings, live-loaded glands, O-ring backups, and optional bellow seals meet ISO 15848 tightness classes, while metal-seated wedge and slab designs handle abrasive solids. Maintenance in place is another industrial benefit—top-entry slab valves allow seat replacement without cutting the line, backseat bushings permit repacking under pressure, and injection fittings let operators add sealant without shutdowns. These choices lower both downtime and spare parts spending on water, steam, gas, and chemical services.
Contact Us
Contact Person: George
Email: [email protected]
Tel/WhatsApp: 13863633883
Website: https://www.es-fire.com